Shuttle Conveyors for Industrial Material Handling
KEYSTONE CONVEYOR designs and builds custom shuttle conveyors for bulk materials distributed across multiple discharge locations. Explore equipment configured around your process, plant layout, and material-handling requirements.
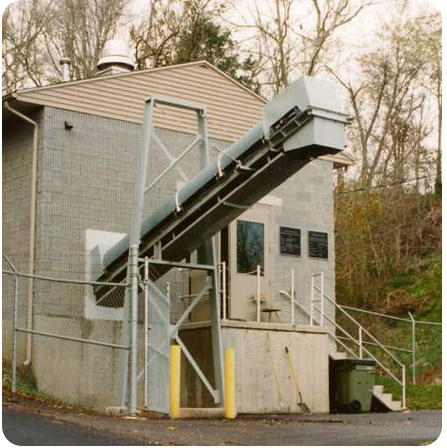
Custom Shuttle Conveyors Built for Your Application
Keystone Conveyor Corporation designs, builds, and delivers shuttle conveyors for industrial and municipal material-handling projects. The right equipment depends on material characteristics, required capacity, available space, and how the system connects to upstream and downstream processes.
Whether you are planning new equipment or replacing an outdated installation, our team can discuss your operating conditions and develop a configuration suited to your project. Share your material, flow requirements, and site constraints to start the conversation.
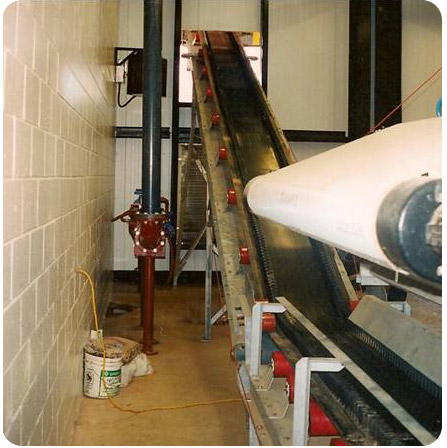
Shuttle Conveyors Applications
These systems can be considered for applications such as:
- Multiple storage bins
- Stockpile distribution
- Process-line feeding
- Multi-point loading
SHUTTLE CONVEYORS Features & Capabilities
Explore six practical features and planning considerations relevant to shuttle conveyors. The final equipment arrangement depends on the material, process, and installation requirements.
Travel Path
Define how the conveyor moves between discharge positions.
Discharge Locations
Identify required receiving points and spacing.
Travel Guidance
Consider rails or guidance arrangements for repeatable movement.
Material Feed
Plan continuous or intermittent loading during shuttle operation.
Control Interface
Review how movement is coordinated with upstream equipment.
Clearance Envelope
Allow space for travel, guarding, and inspection.
Why Choose Keystone for Shuttle Conveyors?
- Flexible discharge positioning
- Efficient distribution
- Reduced fixed transfer points
- Custom design for new installations and retrofit projects
- Equipment planned around your upstream and downstream processes